
 Spanish
 English
 Arabic
 French
 German
 Italian
 Russian
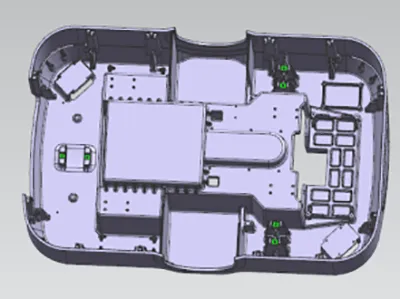
Case Overview
This case involves a robot base, an important load-bearing structural component of collaborative robots and industrial robots.
The robot base connects the robot body to the mounting base and withstands the robot’s own weight, working loads, motion-induced inertia, and vibration loads during operation. Therefore, it has high requirements for structural rigidity, dimensional accuracy, and long-term stability.
The product is die-cast from ADC12 aluminum alloy and then undergoes machining, powder coating, assembly, and other processes. Due to its large size, heavy weight, and complex structure, the product places high requirements on die casting equipment capacity, mold design, and subsequent machining control.
Part Information
| Item | Parámetro |
| Part Name | Robot Base |
| Application Industry | Robotics Industry |
| Material / Grade | ADC12 Aluminum Alloy |
| Product Dimensions | 755 × 499 × 239 mm |
| Product Weight | 20 kg |
| Manufacturing Process Combination | Die Casting + Machining + Powder Coating + Assembly |
| Surface Treatment Process | Powder Coating |
| Quality Inspection | CMM Inspection, X-ray Inspection, Vibration Testing, Static Analysis |
Project Difficulties and Technical Challenges
Core Challenge 1: Complex Structure, Uneven Wall Thickness, and High Forming Difficulty
The robot base measures 755 × 499 × 239 mm and weighs approximately 20 kg, making it a large and complex aluminum alloy structural component.
The product structure includes robot mounting surfaces, reinforcing ribs, connecting bosses, and multiple mounting holes, with significant differences in wall thickness across different areas:
- Reinforcing ribs and thin-wall areas require rapid and complete filling of molten aluminum;
- Thick areas such as the mounting base and connecting bosses are prone to forming hot spots;
- Different solidification rates between thick and thin sections increase the risks of shrinkage porosity, deformation, and dimensional deviation.
Therefore, the product must not only achieve complete forming but also ensure stable production of the large structural component through proper mold design and process control.
Core Challenge 2: Four Large Slides with Core Pulling and Complex Mold Structure
The interior and sides of the robot base contain multiple lateral holes, mounting bosses, and reinforcing structures. Some areas cannot be formed directly through conventional mold opening and closing and therefore require multi-directional core-pulling structures.
The four large slide core-pulling structures present the following challenges:
- Multiple sets of slides need to operate synchronously to avoid uneven forces on the product during demolding;
- Slide positioning accuracy directly affects product dimensions and assembly quality;
- The mold is subjected to significant expansion force during die casting, requiring reliable slide locking;
- Stable mold operation must be maintained during long-term production.
Therefore, the complex slide core-pulling structure is a key challenge in achieving stable mass production of this robot base.
Core Challenge 3: Large-Size Heavy-Duty Structure with High Strength and Rigidity Requirements
As the main load-bearing structure of the robot, the robot base needs to withstand:
- The weight of the robot body;
- Static loads generated by the working load;
- Inertial loads generated during motion;
- Vibration loads generated during high-frequency operation.
If the structural rigidity is insufficient, the mounting stability of the robot will decrease, affecting positioning accuracy and operational reliability.
Therefore, the product must not only meet die casting forming requirements but also ensure structural strength and dimensional stability in critical load-bearing areas.
Solution
To address the challenges of large structural forming, complex core pulling, and load-bearing reliability of the robot base, this project adopted a comprehensive manufacturing solution of mold flow analysis optimization + four-slide core-pulling mold + 2500T-class die casting equipment + dedicated tooling and performance verification to ensure stable production of the large robot base.
1. Mold Flow Analysis to Optimize Mold Design
To address the large size and significant wall thickness variations of the robot base, mold flow analysis was used during the mold development stage to predict filling, solidification, and defect risks.
The main optimization measures include:
- Analyzing molten aluminum flow paths and optimizing the gating system design to avoid local incomplete filling and cold shuts;
- Predicting solidification in thick sections and optimizing feeding and cooling solutions to reduce the risk of shrinkage porosity;
- Optimizing venting and overflow structures to reduce porosity defects;
- Adjusting the mold structure based on simulation results to improve trial mold success rate and mass production stability.
Through preliminary process analysis, the number of mold trials was reduced and the forming stability of large complex components was improved.
2. Four-Slide Core-Pulling Mold + 2500T-Class Die Casting Equipment
For the multi-directional lateral structures of the robot base, this project adopted a mold design with four large slide core-pulling mechanisms and matched it with 2500T-class die casting equipment for production.
The main measures include:
- Using multi-directional slides to achieve stable forming of lateral holes, mounting bosses, and complex structures;
- Optimizing slide positioning, locking, and motion control to ensure mold stability during high-pressure die casting;
- Using 2500T-class equipment to provide sufficient clamping force and injection capacity to meet the production requirements of 20 kg-class large aluminum alloy components.
The combination of large-scale equipment and a dedicated mold solved the forming challenges of the large and complex robot base.
3. Dedicated Machining Tooling + Full-Process Quality Verification
To meet the high load-bearing and assembly accuracy requirements of the robot base, this project adopted dedicated tooling and a multi-dimensional inspection system for quality control.
The main measures include:
- Designing dedicated machining fixtures to ensure the dimensional accuracy of critical features such as robot mounting surfaces and connecting holes;
- Controlling clamping force during machining to reduce the risk of deformation of large aluminum alloy components;
- Using CMM measurement to verify dimensional accuracy;
- Using X-ray inspection to inspect internal quality;
- Combining vibration testing and static analysis to verify structural stability and load-bearing capacity.
These measures ensure that the robot base meets the requirements for strength, rigidity, and long-term reliability under actual operating conditions.
Case Results
Through mold flow analysis optimization, four-slide core-pulling mold design, matching with 2500T-class die casting equipment, and full-process quality control, this project successfully achieved mass production of the large and complex robot base.
| Project Result | Implementation Method | Achieved Result |
| Stable Forming of Large and Complex Robot Base | Mold flow analysis was used to optimize gating, venting, and solidification solutions and improve the filling and solidification process of the large structural component | Achieved stable production of the 755 × 499 × 239 mm, 20 kg-class aluminum alloy robot base, reducing the risks of incomplete filling, shrinkage porosity, and deformation |
| Reliable Forming of Complex Lateral Structures | Adopted a four-slide core-pulling mold structure and optimized slide positioning and motion control | Achieved integrated forming of lateral holes, mounting bosses, and reinforcing structures to meet complex structural assembly requirements |
| Load-Bearing Performance and Structural Reliability Verification | Combined CMM measurement, X-ray inspection, vibration testing, and static analysis for comprehensive verification | Ensured that product dimensional accuracy, internal quality, and load-bearing performance met robot operating requirements |
| Complete Manufacturing Process Delivery Capability | Combined 2500T-class die casting equipment with machining, powder coating, and assembly processes to achieve full-process manufacturing | Completed batch delivery from die-cast blanks to complete robot base assemblies |
